 English

A Lifecycle Maintenance Plan for High-Current Slip Rings in Coating Machinery Treat commissioning data as the maintenance baseline Maintenance starts before production. Record the approved circuit schedule, terminal identification, mounting alignment and cable routing when the system is commissioned. For the source configuration, the reference architecture includes 180 A, 40 A and 10 A groups, […]
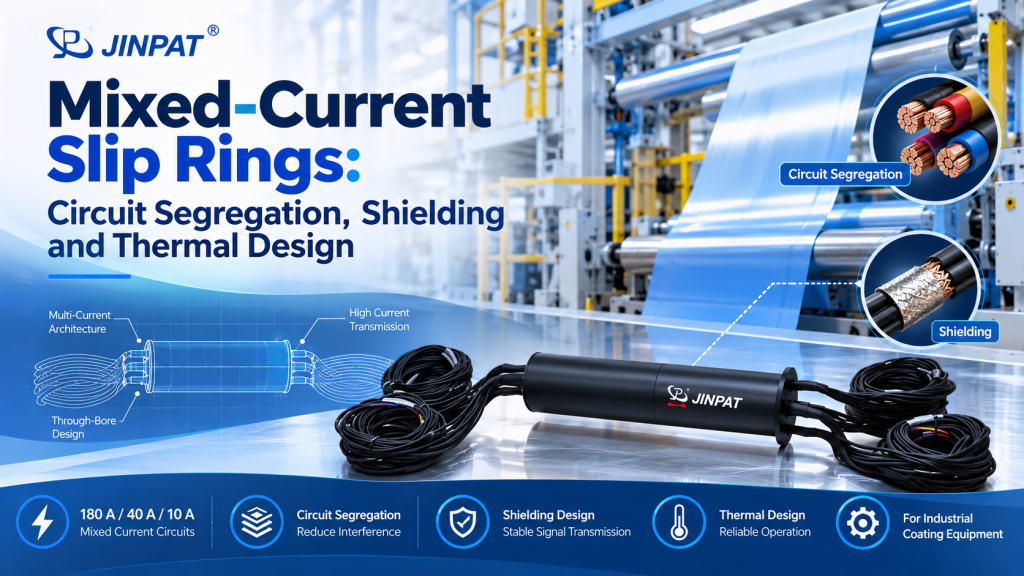
Maintenance starts before production. Record the approved circuit schedule, terminal identification, mounting alignment and cable routing when the system is commissioned. For the source configuration, the reference architecture includes 180 A, 40 A and 10 A groups, a 50 mm through bore and a listed maximum working voltage of 440 V. The released drawing for the installed unit must replace these preliminary values in the plant record.
Measure point-to-point continuity and any resistance values specified by the supplier. Capture representative temperatures under normal production load. Photograph cable supports, shield terminations and the anti-rotation arrangement. These records make later changes easier to identify.
Operators can identify many developing problems without opening the unit. Add a short visual and operational check to the machine routine: unusual noise, vibration, odor, discoloration, loose cables, damaged strain relief or abnormal housing temperature. The inspection frequency should follow the approved manual and the machine duty cycle.
Do not assume that a slip ring is maintenance-free. Even when the internal contact system requires little routine intervention, the surrounding cables, fasteners, ventilation and terminals still need inspection.
Isolate and verify the equipment according to the plant’s safety procedure. Inspect accessible terminals for looseness, contamination or heat marks. Compare specified resistance or insulation measurements with commissioning values and supplier limits. A trend is often more useful than a single number, provided the same method and conditions are used.
Check mounting fasteners, alignment, cable bend radius and strain relief. Confirm that the stationary side is restrained correctly and that no external structure is forcing the slip ring out of alignment. Inspect the central bore area for contact with the shaft, pipe or protective sleeve.
Coating lines often have expensive interruptions because cleaning, web handling and process restart take time. Combine slip-ring checks with existing planned shutdowns where practical. Use operating hours, revolutions and load history to determine the interval rather than relying on calendar time alone.
If the machine frequently runs near its current limit, include temperature trending. If the load pattern changes, review the circuit schedule and thermal assumptions before treating the new recipe as equivalent to the original one.
For plants with long logistics routes, maintain the released drawing, wiring diagram, approved replacement code, terminal hardware list and supplier contact details in the maintenance system. Decide whether the complete slip ring, wear parts or only external connection items should be held as spares. The choice depends on lead time, repair capability and downtime cost.
The public model and project code should remain removed from marketing pages, but the internal maintenance record must retain the exact approved identification so the replacement matches the installed configuration.
Transport or storage in cold regions does not prove that the installed product is rated for low-temperature operation. Ask the supplier for storage limits, condensation precautions and the permitted temperature before energizing or rotating. Allow equipment to stabilize when required and inspect for moisture after temperature transitions.
A documented lifecycle plan turns the slip ring from an opaque component into a maintainable machine subsystem. It also prevents unverified lifetime claims from replacing real condition data.
JINPAT photovoltaic slip rings have high quality and competitive price. JINPAT has provided hundreds of models of electro-optical rotary joints for both civil and military industries. Most of JINPAT electro-optical slip rings have high transmission capacity. High-end slip rings can transmit 4K@60FPS high-definition video signals. OVERVIEW Design product sketches and models using SOLIDWORKS 3D Computer […]
With many years of experience in managing various types of projects, the management team of JINPAT is able to eliminate all obstacles that arise during the execution of projects to ensure that the technology is followed and the products are manufactured successfully. In addition, JINPAT understands the importance of good documentation. Documents such as certificates […]
JINPAT carries out precision machining of all components of its products. At all stages of production, from drawing to molding, JINPAT is committed to being precise and ensuring that the best slip rings are produced. With the ability to machine parts to a tolerance of 5 microns, our experienced, highly skilled team uses the latest […]
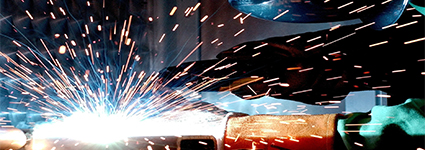
JINPAT welding technicians are experts in Gas Metal Arc Welding (GMAW), Flux Cored Arc Welding (FCAW), Gas Tungsten Arc Welding (GTAW) and Semi Metal Arc Welding (SMAW). They are dedicated individuals who value precision and aesthetics in the production of machine components. OVERVIEW Welding procedures comply with codes such as ASMEIX, AWS, DIN, API, B31.1, […]
JINPATElectronics is a customer-oriented corporation. We do our utmost to provide our customers with high-standard solutions for transmission including rotation. Up to now, JINPAT has provided its services to more than 10,000 customers worldwide. Each slip ring produced by JINPAT undergoes a series of rigorous and systematic inspections and durability tests before being delivered to […]
With advanced testing and measuring devices, JINPAT’s Quality Control Department conducts systematic inspections of our products. Our quality measurement system complies with ISO 9001:2015. JINPAT has great confidence in its products and has earned a good reputation for producing products of unrivaled quality. REVIEW Detailed inspection and provision of data in the form of documentation […]